Services
- EDM/WEDM machining services
- EDM/WEDM machine maintenance and inspections for ZAPbp (Zakład Automatyki Przemysłowej B.P.) machines as well as in-house machines
- Training on operation of ZAPbp and in-house EDM/WEDM machines
- EDM machine modernization for ZAPbp production
- Replacement of control system with PLC (PP15ster) enabling machining along any straight path in the workspace and along any XY arc (particularly useful for EDM threading)
- Replacement of lead screws with HIWIN ball screws (optionally combined with ACservo drive replacement)
- PCB design
- Based on technical documentation provided by the client
- As part of creating a prototype of the device
- Firmware development. Delivering projects based on controllers using ARM-core microcontrollers (Cortex-M0, M3, M4). Embedded software (depending on project complexity) is implemented as:
- Applications developed in C
- Applications developed in C/C++ based on real-time operating systems: FreeRTOS, RTX, or RTX5
- 3D Printing Services using FDM Technology
- Maximum print size: 220×220×250 mm
- Supported filaments: PLA, PETG, ABS, ABS kevlar, TPU
Knowledge base
EDM (Electrical Discharge Machining) is a process designed to reproduce the shape of an electrode (a tool made of copper or graphite) in an electrically conductive workpiece (the eroded material). The electrical erosion process is based on generating high-current electrical discharges occurring between the electrode and the workpiece in a dielectric environment. Therefore, there must always be a certain working gap (from 0.05 mm to 0.1 mm) between the surfaces of the electrode and the workpiece – the process takes place “without contact”, meaning there is no mechanical contact between the tool and the workpiece. In the case of sinker EDM machines, the dielectric is most commonly a liquid produced from highly purified petroleum fractions.
Electrical Discharge Erosion
In order to describe the stages of occurrence or development of a single discharge, it is first necessary to know what type of current block is being used. In most cases, this type determines the default electrode/workpiece polarity, which in turn defines which current (ionic or electronic) will have the dominant influence on the EDM process.
- The electrode approaches the workpiece to the “ignition” distance, i.e. the distance at which a spark can occur,
- The power transistors in the current block are switched on, causing a high voltage to appear on the electrode,
- As a result of the large potential difference between the electrode and the workpiece, an electromagnetic field is created between them. Its intensity is greatest where the distance between the workpiece and electrode surfaces is smallest (it should be remembered that no surface is perfectly flat – it always has microscopic protrusions and depressions). In the area of the highest field intensity, the dielectric liquid becomes polarized to a level at which the resistance of that area drops to a “critical” value, allowing current to flow,
- The discharge begins with the ignition of an electron arc, i.e. the emission of electrons from the workpiece material and their movement towards the electrode,
- The cloud of electrons colliding with dielectric molecules (hydrocarbon chains) causes them to break down into hydrogen and carbon molecules. At a later stage, an electron is “stripped” from the hydrogen atoms, resulting in the appearance of “free” protons in the discharge space, i.e. positively ionized particles. Accelerated by the electromagnetic field, these protons begin to move towards the workpiece, forming an ionic arc. Since the discharge space contains a cloud of “free” electrons and protons, a plasma channel is formed,
- The positively charged ions accelerated by the electromagnetic field collide with the surface of the workpiece, transferring their kinetic energy to the workpiece, where it is converted into thermal energy. Localized melting of the workpiece material occurs, with the local temperature rising to as much as 14,000°C,
- As the temperature increases in the discharge area, a bubble of vaporized dielectric forms around the plasma channel,
- The power transistors in the current block are switched off, causing the flow of electrons to stop,
- Due to the very large pressure difference between the surroundings and the inside of the bubble containing vaporized dielectric, the bubble implosively collapses inward. As a result, the locally molten workpiece material is ejected into the dielectric, where it forms into almost perfectly spherical particles,
- The dielectric is re-ionized.
The next discharge occurs at another location that is, at that particular moment, the most optimal one… and this is how the specified volume of workpiece material is gradually removed.
Applications of EDM
Where is EDM used today? Due to the low productivity of the process compared with other conventional machining methods (such as milling or turning), it is primarily used where everything else fails, namely:
- for precision machining of difficult-to-cut materials such as titanium alloys, hardened steels, cemented carbides and other modern alloys (e.g. Inconel),
- when the machining process must be non-contact, which minimizes the risk of cracking or deformation of the workpiece,
- for producing deep, narrow and complex cavities (in injection molds or dies) that cannot be accessed with a milling cutter,
- for non-standard machining operations such as producing threads in difficult-to-cut materials or profiling the working surfaces of diamond/CBN wheels,
- when minimizing the depth of changes to the internal structure of the material is important to us (similarly to laser cutting or plasma cutting, EDM is based on melting the material. However, unlike these other methods, the material is melted to a depth of no more than 0.2 mm. Therefore, if the workpiece material is hardenable, only a thin outer layer will become hardened).
The electrical discharge erosion process is based on generating high-current electrical discharges occurring between the electrode and the workpiece in a dielectric environment. EDM operating parameters are therefore primarily related to controlling the transistor-based current block, whose power output is connected to the electrode. The control system sends a rectangular clock signal to the pulse generator, determining how long the power transistors are switched on/off, thereby enabling/blocking the flow of current between the electrode and the workpiece. Thus, we have three basic settings:
- pulse duration: the duration of the discharge,
- pause duration: the duration of the interval between consecutive discharges,
- current: the amplitude of the current flowing through the plasma channel during the discharge,
These parameters allow us to influence machining efficiency, surface roughness, electrode wear and the size of the lateral gap.
Additionally, we have auxiliary parameters responsible for the stability of the machining process: working threshold and short-circuit threshold (specified in %).
EDM Machining Efficiency
The basic characteristic describing the operation/behavior of the current block is its machining efficiency characteristic. Below is an example plotted for the following conditions:
- Workpiece material: ST steel
- Dielectric: cosmetic-grade kerosene
- Electrode: copper (M1E) rod, diameter ø16 (S≈200mm2)
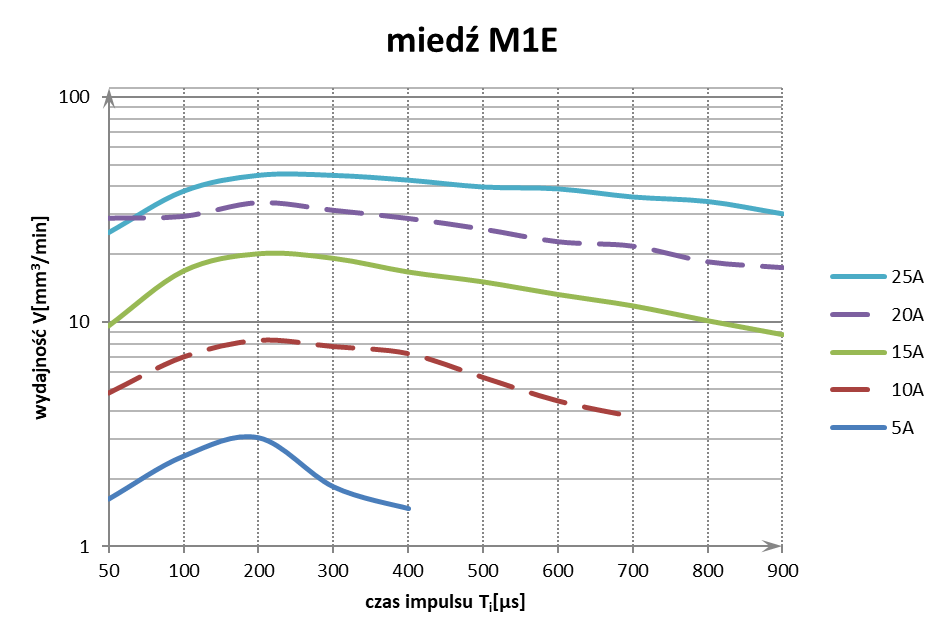
The data used to plot the above characteristic were normalized to continuous operation conditions (without the use of periodic electrode lifting). The general conclusions drawn from their analysis are as follows:
- Increasing the current value increases machining efficiency (the higher the current, the greater the volume melted from the workpiece during a single discharge),
- Increasing the pulse duration increases machining efficiency until a certain maximum is reached,
- The pulse duration at which the highest efficiency is achieved for individual current settings oscillates around Ti=200μs
Surface Roughness
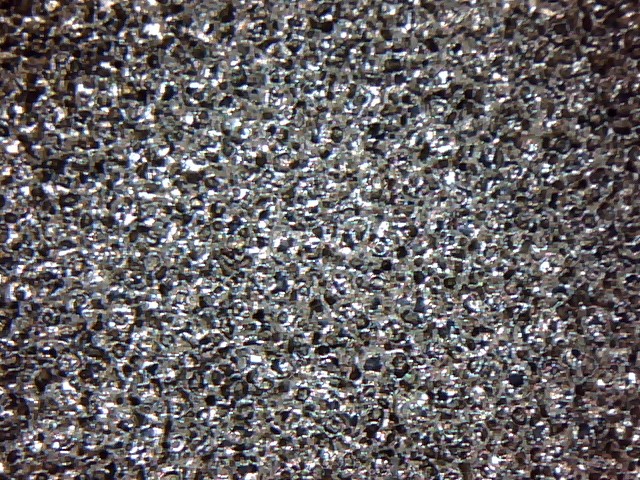
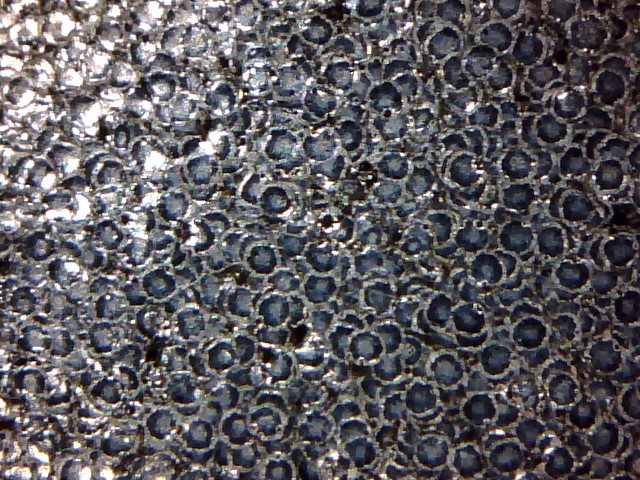
The Ra surface roughness characteristics as a function of pulse duration have a shape similar to the efficiency characteristics:
- Increasing the current value increases surface roughness,
- Increasing the pulse duration increases surface roughness until a certain maximum is reached, after which the roughness decreases due to the appearance of “smeared craters”.
For I=5A; Ti=200us:
For I=5A; Ti=900us:
Electrode Wear
The wear of a copper electrode depends on:
- melting of the electrode material, resulting from a mismatch between the average current density flowing through the electrode and its ability to dissipate heat. As a practical “workshop conversion factor” for EDM, we conventionally assume 0.2A/mm2. In reality, electrode wear resulting from melting of the electrode material is primarily influenced by its shape and volume, followed by such settings as current, pulse duration and pause duration. Taking an electrode with a working surface area of 28mm2 (which conventionally gives us the possibility of setting a maximum of 5.6A) and setting the current to 20A, we will obtain different effects depending on whether the electrode is a cylinder with a radius of 3mm or a rectangular prism with a base of 0.5×56mm. In the first case, we will observe wear of the edges without wear of the “front face”. In the second case, the electrode will wear by 50%,
- the number of discharges required to erode a given volume – the fewer discharges that occur, the lower the electrode wear. Here, we primarily consider the moment when the current arc is initiated – the “cleaner” the initiation is (free from relaxation oscillations and unwanted current “spikes”), the better the electrode life. Each discharge (for electrode (+), workpiece (-) polarity) begins with the ignition of an electron arc, i.e. the emission of electrons from the workpiece material and their movement towards the electrode. Accelerated in the electromagnetic field, the electrons collide with the surface of the electrode material, transferring part of their kinetic energy to it, where it is converted into thermal energy. Localized melting of the electrode material occurs, which in turn causes its erosion.
Setting the “current” parameter with regard to electrode wear represents a balance between two causes of electrode degradation. If the current is too high, the electrode will undergo excessive melting. If it is too low, a greater number of discharges will be required to remove the specified volume, exposing the electrode to greater erosion caused by the ignition of electron arcs.
Pause Duration
The pause duration between pulses is required to properly extinguish the preceding discharge and cool the area surrounding it to a temperature below 180˚C (this is the lower boiling point limit of cosmetic-grade kerosene; falling below this temperature is necessary for the process to proceed correctly). Shortening the pause duration directly increases machining efficiency, but if its value is too low and flushing of the gap is ineffective, it may lead to the occurrence of so-called “burn marks”.
Working Threshold and Short-Circuit Threshold
To explain what these two “mysterious” settings are, we should first note that the only significant difference between an EDM control system and those used in other CNC machines is the presence of a so-called “spark control” system. This system provides feedback to the PLC controller, based on which the controller determines whether it can move the machine's working head at the set speed, whether it should stop, or whether it should even retract, all in order to maintain an appropriate gap between the electrode and the workpiece. The “spark control” system generates feedback based on statistical analysis of the potential difference between the electrode and the workpiece for a specified number of “pulses” (in this case understood as the number of periods during which the power transistors in the current block are switched on, i.e. the number of periods during which a discharge may occur). Assuming that the power transistors are switched on one hundred times within a given period, each such “switch-on” may result in one of three states: no discharge, a proper discharge occurs, or a short circuit occurs (i.e. physical contact between the electrode and the workpiece). The occurrence of each of these states is counted and then compared with the values specified by the settings. If 30 proper discharges occur out of 100 specified “pulses”, and the operator has set the “working threshold” to 20%, the PLC controller will receive information that it should stop the movement of the working head due to an excessive frequency of discharges. A similar situation applies to the “short-circuit threshold”: if 30 detections of contact between the electrode and the workpiece occur out of 100 specified “pulses”, and the “short-circuit threshold” is set to 20%, the PLC controller will receive information that it should retract the working head until the short circuit is cleared.
The working threshold acts as a kind of “muzzle” for the machine – if more discharges occur within a given unit of time than the specified threshold, this means that there is too much material to be removed for the working head to move to the next point of the programmed trajectory. In such a situation, the machine should stop and wait until the number of discharges falls below the specified threshold. If the working threshold is set too low, machining efficiency decreases. If it is set too high, process stability is lost (the machine moves too quickly along its trajectory, resulting in frequent short circuits), additionally increasing the risk of so-called “burn marks”.
The short-circuit threshold, on the other hand, determines how sensitive the machine should be to detecting contact between the electrode and the workpiece. During the machining process, erosion products in the form of small particles of eroded material are generated between the electrode and the workpiece. As they accumulate in the working gap (before being removed by the flushing flow of the dielectric), they may cause short circuits between the electrode and the workpiece. Such events should not affect process stability, so in order to eliminate their influence, we increase the short-circuit threshold, thereby making the machine less sensitive to the occurrence of accidental short circuits.
Setting the Operating Parameters
Setting the operating parameters to achieve maximum EDM efficiency while minimizing electrode wear:
- Determine the maximum current value using the formula I=J∙S, where: S – electrode working surface area, J – limiting current density (for copper J=0.2A/mm2; for graphite J=0.3A/mm2),
- Determine the pulse duration based on the efficiency characteristic,
- The pause duration should not be shorter than tp=Ti/10,
- when machining a material with a high zinc content, tp should not be shorter than Ti/5,
- as flushing conditions deteriorate or in the case of a very small machining area (<10mm2), the pause duration should be increased,
- Set very strong flushing from above for cavities deeper than 5mm.
Contact
Email: poterala.piotr@gmail.com
Phone: +48 507-493-844
Address
gen. Maczka 19/24,99-300 Kutno, Poland
Correspondence address
Bociania 3,99-300 Kutno, Poland
VAT ID: PL7752601355